Heavy-Duty Horizontal Split Case Fire Pump
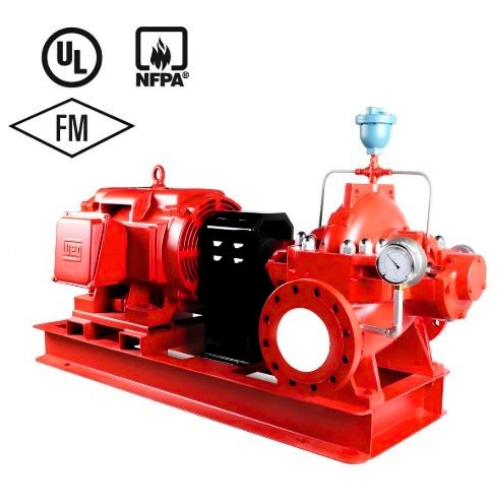
A high-flow water movement is the Heavy-Duty Horizontal Split Case Fire Pump. A well-chosen horizontal split case fire pump can supply the flow and pressure needed by sprinkler, fire suppression, and hydrant networks for fire safety projects. Double-suction horizontal split-case configurations for fire suppression services are included in current fire pump standards and manufacturer literature.
Specifications:
Product Type: Heavy-Duty Fire Pump
Origin: China
Pump Type: Horizontal Split Cas
Approvals: UL-listed and FM-approved
Compliance: NFPA 20
Flow: 300 - 8000 GPM
Pressure: 5 - 33 BAR
Speed: 1470 - 3550 RPM
Temperature Range: -15°C to +120°C
Drive: Electric or Diesel
Capacity: up to 8000 USGPM
Motor Power: 2.2~1800 kW
Power Supply: 3 Phase, 50 / 60 Hz, 380 – 460V
Operation: Advance
Head: yes
Frequency: yes
Casing Material: Cast Iron, Duplex Stainless Steel
Impeller Material: Cast Iron, Duplex Stainless Steel, Bronze
IP Rating: IP55

Features of Horizontal Split Case Fire Pump
- Heavy-duty horizontal split-case construction
- Single-stage centrifugal pumping design
- Double-suction impeller configuration
- High-flow water delivery capability
- Robust casing construction
- Balanced hydraulic design
- Easy-access upper casing arrangement
- Heavy-duty shaft and bearing assembly
- Replaceable wear components on applicable designs
- Baseplate-mounted configuration
- Flexible electric or diesel driver options
- Coupling and coupling-guard arrangement
- Fire protection system compatibility
- Suitable for high-pressure applications
- Wide range of flow and head configurations
- Designed for demanding commercial and industrial duties
- Maintenance-friendly construction
- Available in fire-pump configurations meeting applicable project standards
Horizontal split-case fire pumps commonly use an axially split casing with a double-suction impeller, while the upper casing can be removed to provide access to internal components without disturbing connected piping on applicable designs.
Benefits of Horizontal Split Case Fire Pump
- Convenient Internal Access: The split casing provides practical access to internal components for inspection and servicing. This is one of the major reasons horizontal split-case designs are widely selected for fire suppression applications.
- Balanced Hydraulic Operation: A double suction Horizontal Split Case Fire Pump draws water toward both sides of the impeller. This configuration can provide balanced hydraulic loading and is particularly suitable for high-capacity pumping duties.
- Reliable Long-Term Service: Heavy-duty shafts, bearings, casing construction and properly selected materials can provide dependable service when the pump is correctly installed, operated and maintained.
- Flexible Driver Selection: Depending on the fire protection design, the pump can be paired with an electric motor or diesel engine. Complete fire-pump product lines are available in both electric- and diesel-driven arrangements.
- Easier Maintenance Planning: The accessible split-case construction can simplify inspection and component servicing while reducing the need to disturb connected piping during certain maintenance activities.
Advantages of Horizontal Split Case Fire Pump
- High-capacity water pumping
- Double-suction hydraulic configuration
- Strong mechanical construction
- Practical maintenance access
- Suitable for demanding fire protection systems
- Electric and diesel driver options
- High-flow fire suppression capability
- Suitable for large buildings and industrial facilities
- Flexible installation configurations
- Long-service design potential
- Easy inspection of internal components
- Compatible with dedicated fire pump controllers
- Suitable for hydrant and sprinkler networks
- Adaptable to project-specific hydraulic requirements
Application of Horizontal Split Case Fire Pump
- Fire hydrant systems
- Automatic sprinkler systems
- Fire suppression systems
- Industrial factories
- Garment factories
- Manufacturing plants
- Warehouses
- Power plants
- Commercial buildings
- Shopping malls
- Hospitals
- Hotels
- High-rise buildings
- Petrochemical facilities
- Oil & gas facilities
- Municipal water systems
- Large industrial water networks
- Fire pump rooms
Horizontal Split Case Fire Pump are commonly positioned for applications requiring high-capacity, high-pressure water delivery, including high-rise buildings, large commercial facilities and industrial sites.
Parts of a Horizontal Split Case Fire Pump
The parts of a Horizontal Split Case Fire Pump can vary by manufacturer and model, but a typical assembly may include:
- Pump casing
- Upper casing
- Lower casing
- Double-suction impeller
- Pump shaft
- Shaft sleeves
- Bearings
- Bearing housings
- Stuffing boxes or mechanical seals
- Wear rings
- Coupling
- Coupling guard
- Baseplate
- Suction flange
- Discharge flange
- Pressure gauge connections
- Drain and vent connections
Horizontal Split Case Double Suction Centrifugal Pump
- Horizontal split casing
- Centrifugal hydraulic operation
- Double-suction impeller
Horizontal Split Case Fire Pump Installation
- Proper foundation
- Correct pump positioning
- Accurate shaft alignment
- Adequate suction conditions
- Correct pipe support
- Proper piping alignment
- Appropriate isolation valves
- Correct check-valve arrangement
- Air removal and venting where required
- Proper coupling protection
- Suitable electrical or diesel-driver connections
- Adequate maintenance clearance
Horizontal Split Case Pump Fire Protection
The pump may supply:
- Fire hydrant networks
- Sprinkler systems
- Fire hose systems
- Deluge systems
- Fire suppression networks
Maintenance of Horizontal Split Case
Maintenance activities may include:
- Pump visual inspection
- Leakage inspection
- Bearing condition checks
- Lubrication
- Shaft alignment verification
- Coupling inspection
- Seal or packing inspection
- Wear-ring inspection
- Fastener inspection
- Pressure-gauge checks
- Driver inspection
- Controller inspection
- Performance testing
- Vibration monitoring
Why Choose Heavy-Duty Horizontal Split Case Fire Pump?
The Heavy-Duty Horizontal Split Case Fire Pump offers a strong combination of high-flow capability, robust construction, double-suction hydraulic options and maintenance-friendly access.
Why Choose?
- High-capacity fire water pumping
- Heavy-duty construction
- Double-suction impeller option
- Balanced hydraulic design
- Convenient internal access
- Suitable for demanding fire protection applications
- Electric or diesel driver compatibility
- Flexible flow and pressure selection
- Suitable for large commercial facilities
- Suitable for industrial fire protection
- Compatible with hydrant and sprinkler networks
- Practical maintenance arrangement
- Long-term service potential
- Project-specific configuration
- Available in applicable listed/approved fire-pump configurations
Conclusion
The Heavy-Duty Horizontal Split Case Fire Pump is split casing, double-suction hydraulic configuration, robust rotating assembly and maintenance-friendly construction make it particularly suitable for large-scale fire water applications.
For a complete fire protection solution, the pump should be selected together with the appropriate driver, controller, valves, piping, water source and accessories. Flow, pressure, suction conditions, certification requirements and hydraulic calculations should all be evaluated before final selection. Current manufacturer fire-pump ranges demonstrate the availability of horizontal split-case systems in both electric- and diesel-driven configurations and in NFPA 20/UL/FM-oriented packages.